Industrial & Performance Flooring
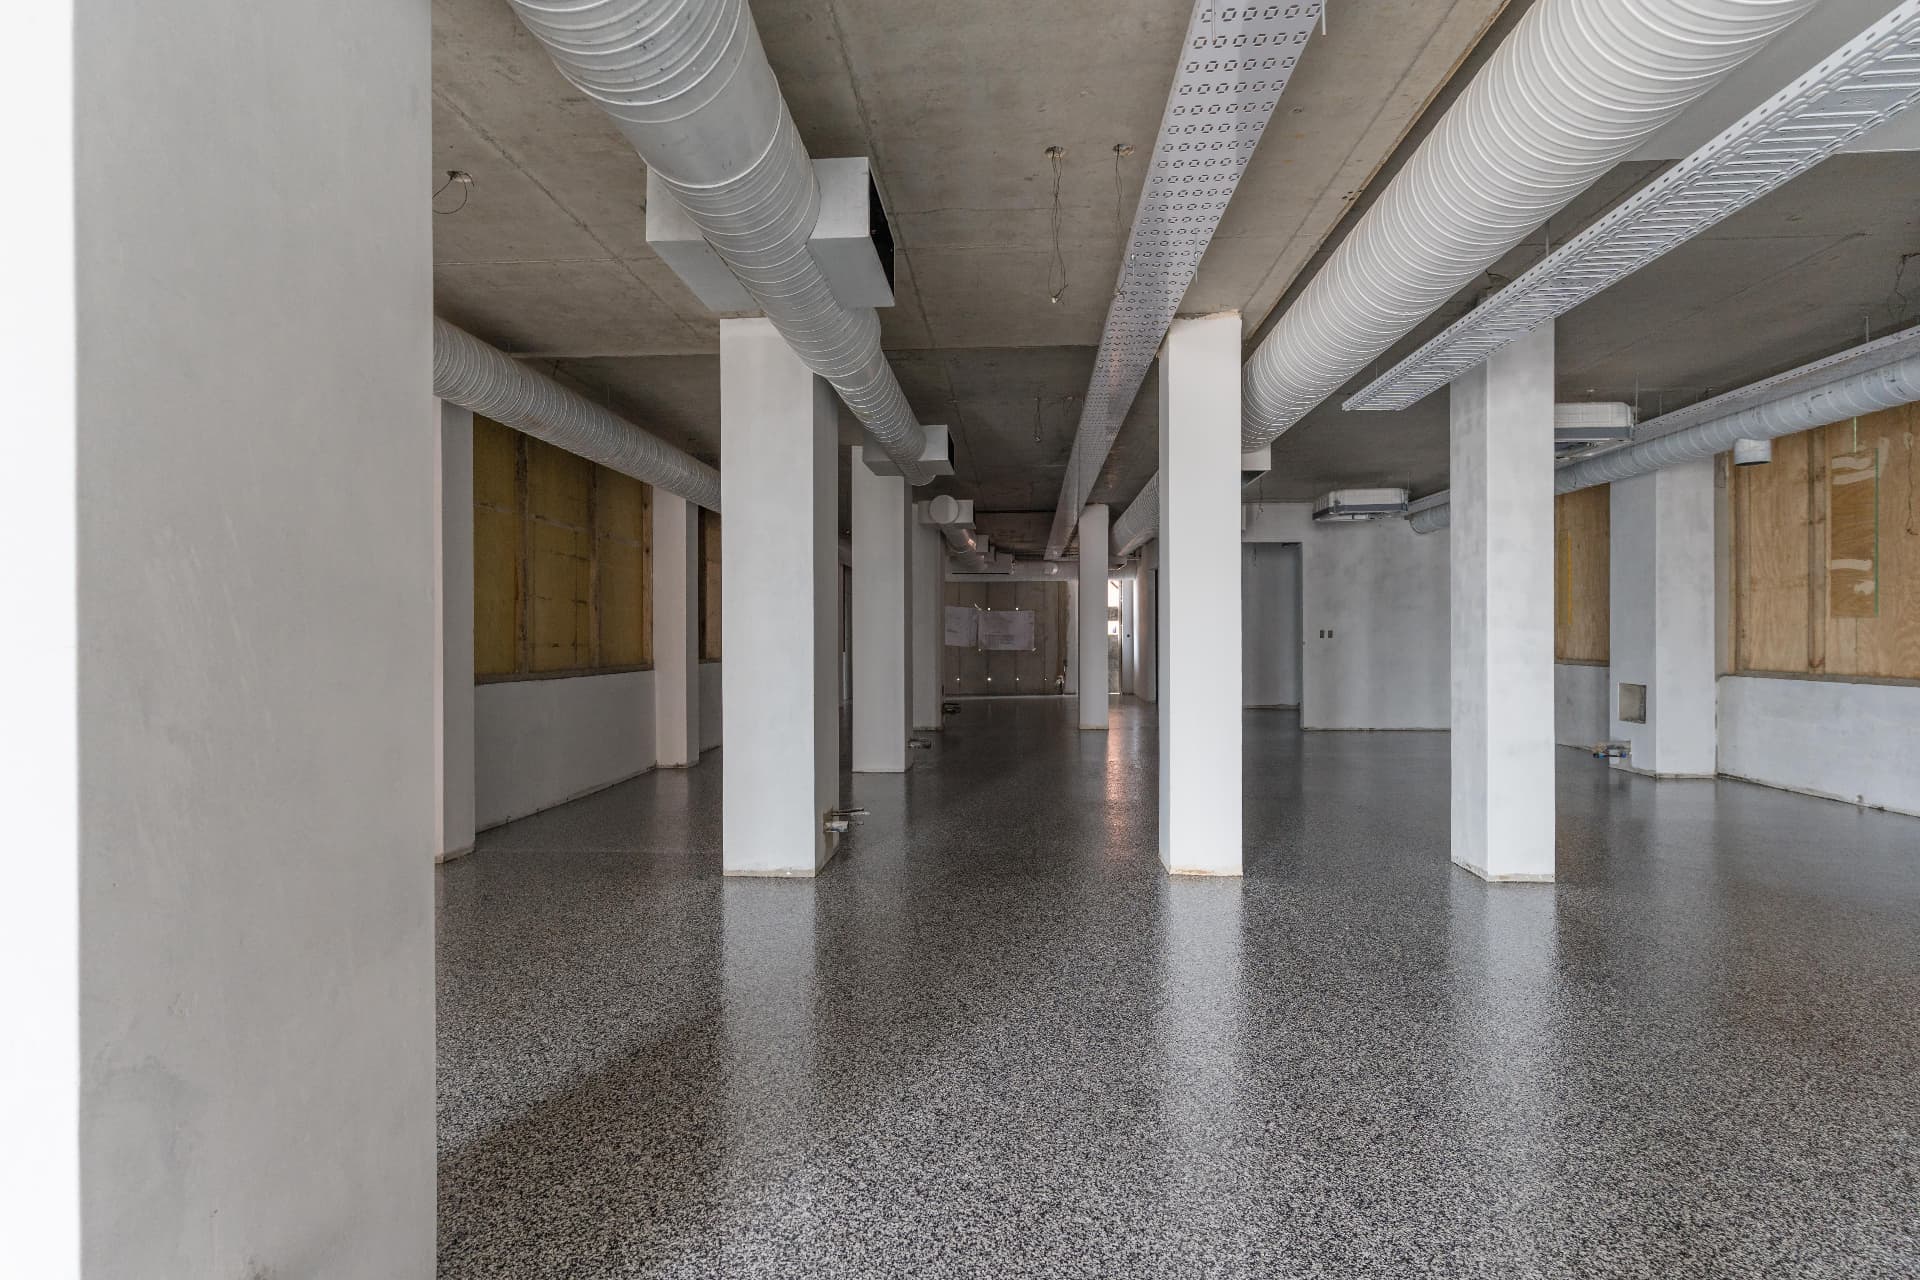
Industrial and commercial flooring systems engineered for hygiene, chemical resistance, abrasion resistance, impact resistance and demanding traffic conditions.
What it solves
Production floors, warehouses and process areas carry forklifts, chemicals, washdowns and heat. A floor that is not matched to those conditions wears, dusts, cracks or becomes a hygiene risk long before it should.
Common Problems
- Chemical attack
- Abrasion
- Forklift traffic
- Thermal shock
- Hygiene
- Slip hazards
- Existing floor degradation
Desired Outcomes
- Longer floor life
- Improved hygiene
- Chemical resistance
- Reduced maintenance
- Safer working environment
Key Benefits
Matched to the exposure
Systems selected according to substrate, traffic, chemical exposure and operational requirements.
Seamless surfaces
Resin and screed systems that reduce joints where dirt and moisture collect.
Range of thicknesses
From thin protective seals to 6mm heavy-duty screeds, as published in each system's data.
Where it is used
- Manufacturing plants
- Warehouses and logistics
- Food and beverage processing
- Workshops
- Process areas
- Commercial back-of-house
Nuvo systems for industrial & performance flooring
Contact us for detailed specifications and technical guidance on these systems.
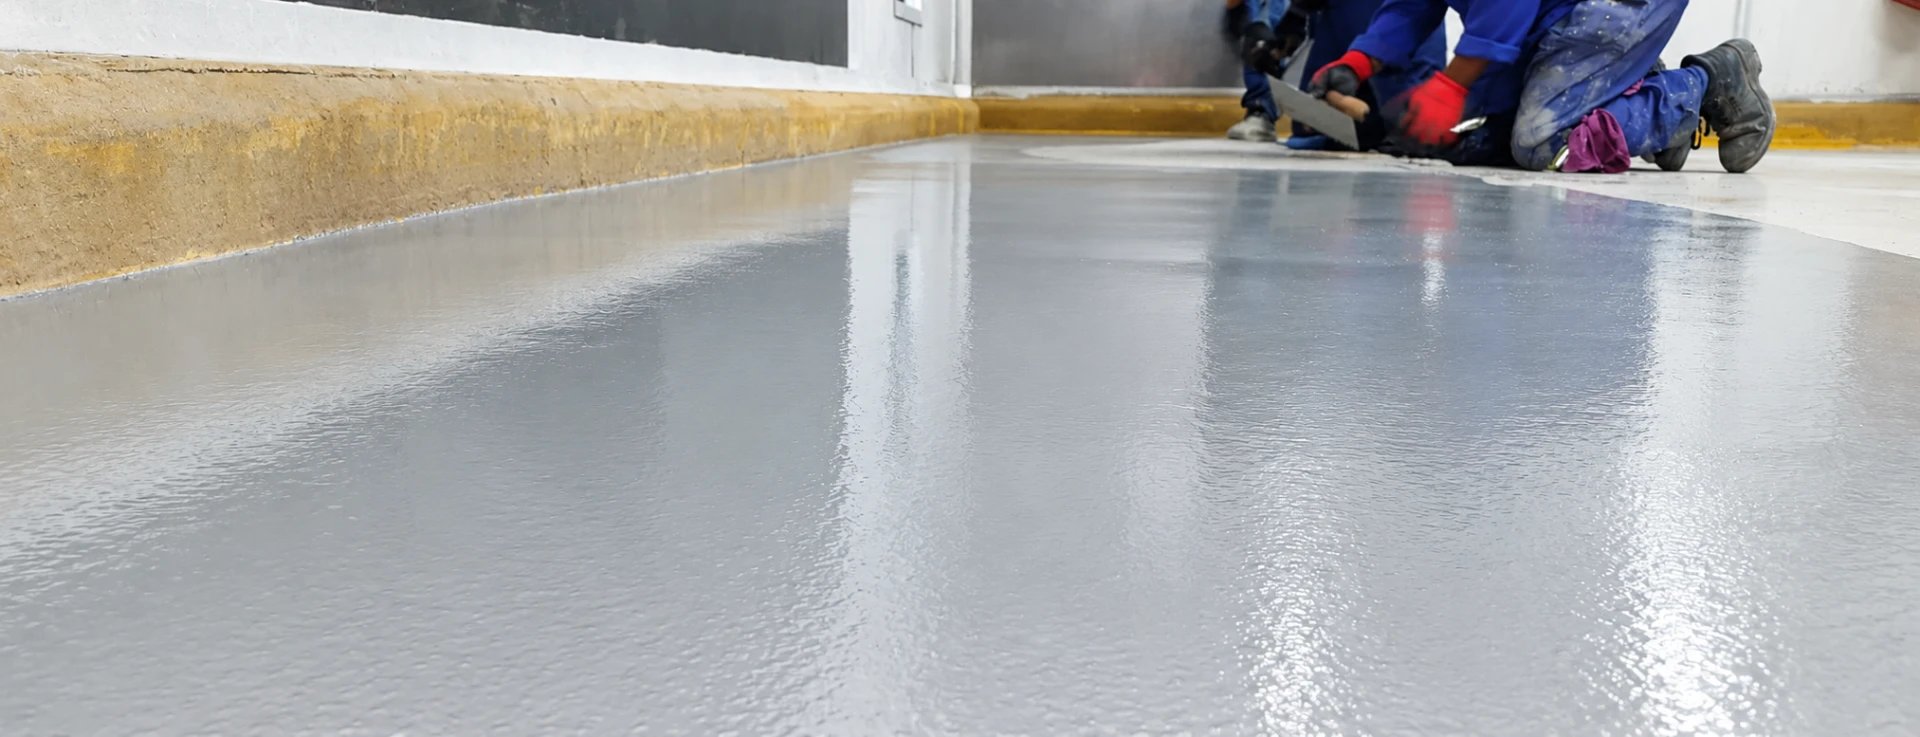
NUVO POLYURETHANE SCREED - 6MM
HIGH PERFORMANCE POLYURETHANE FLOORING SYSTEM
Read More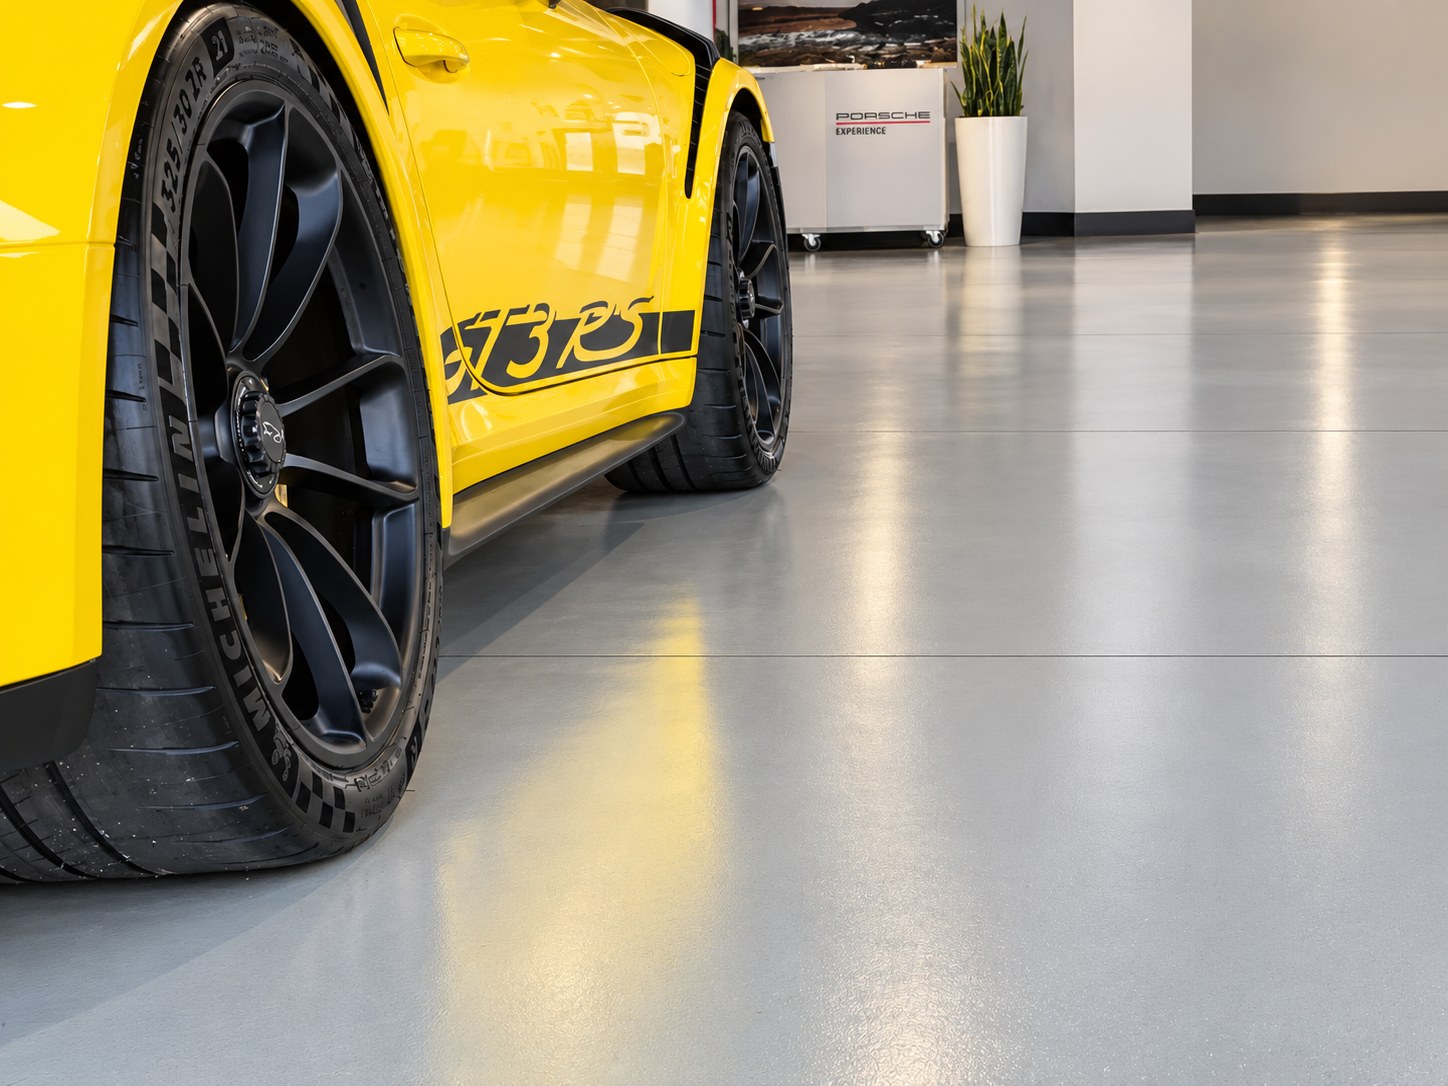
NUVO POLYCRETE 6MM
HIGH PERFORMANCE POLYURETHANE SCREED FLOORING SYSTEM
Read More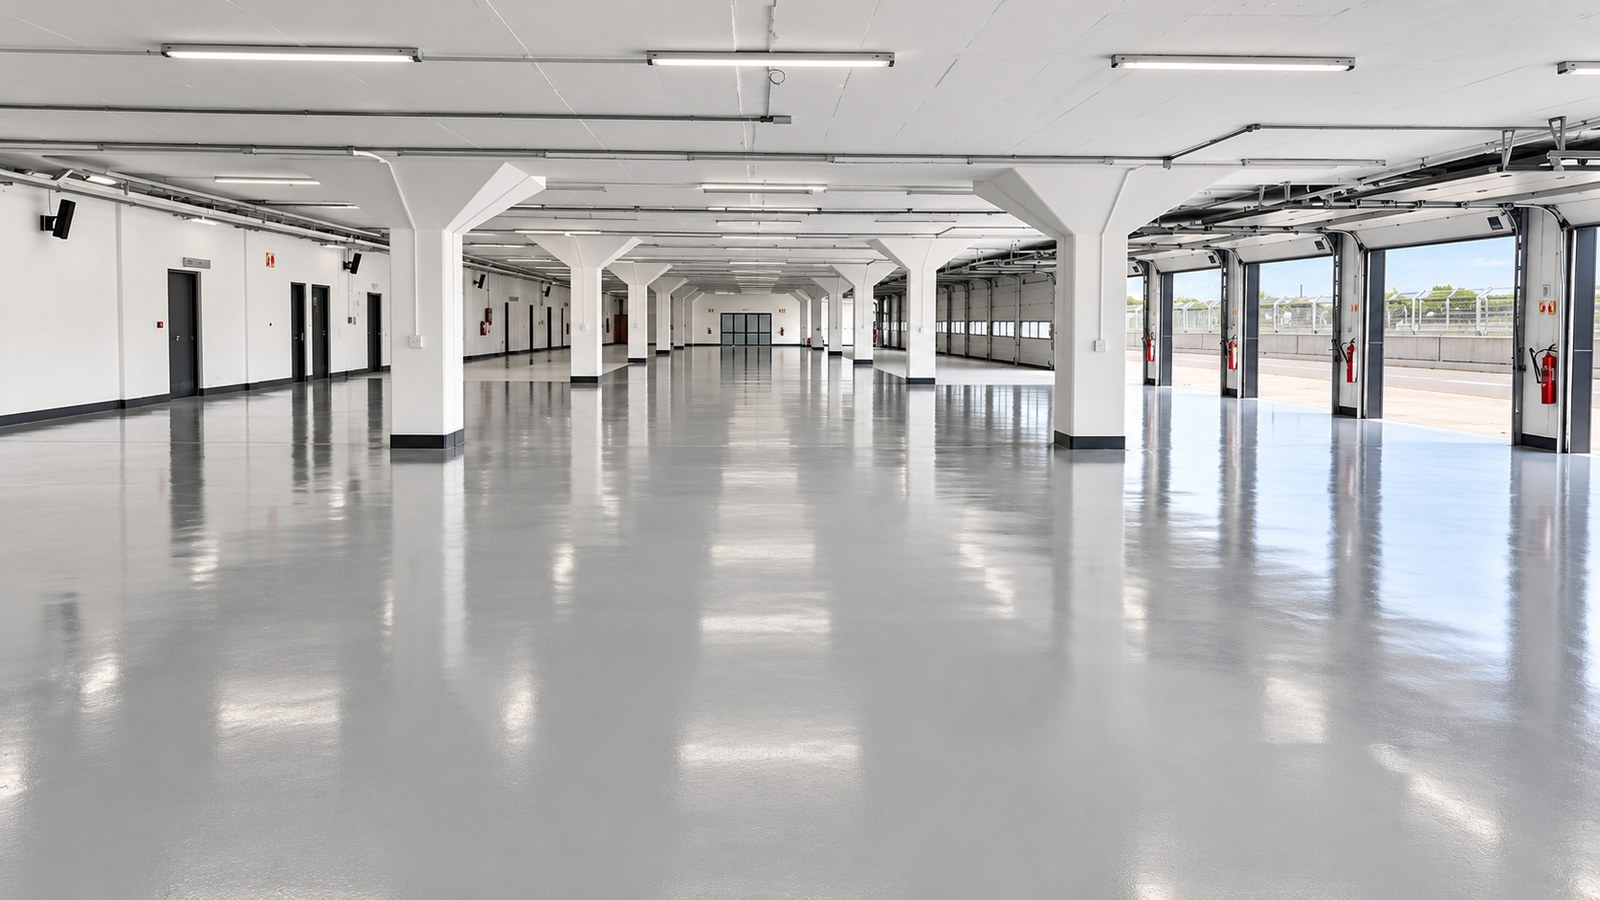
NUVO POLYCRETE 3-4MM
HIGH PERFORMANCE POLYURETHANE FLOORING SYSTEM
Read More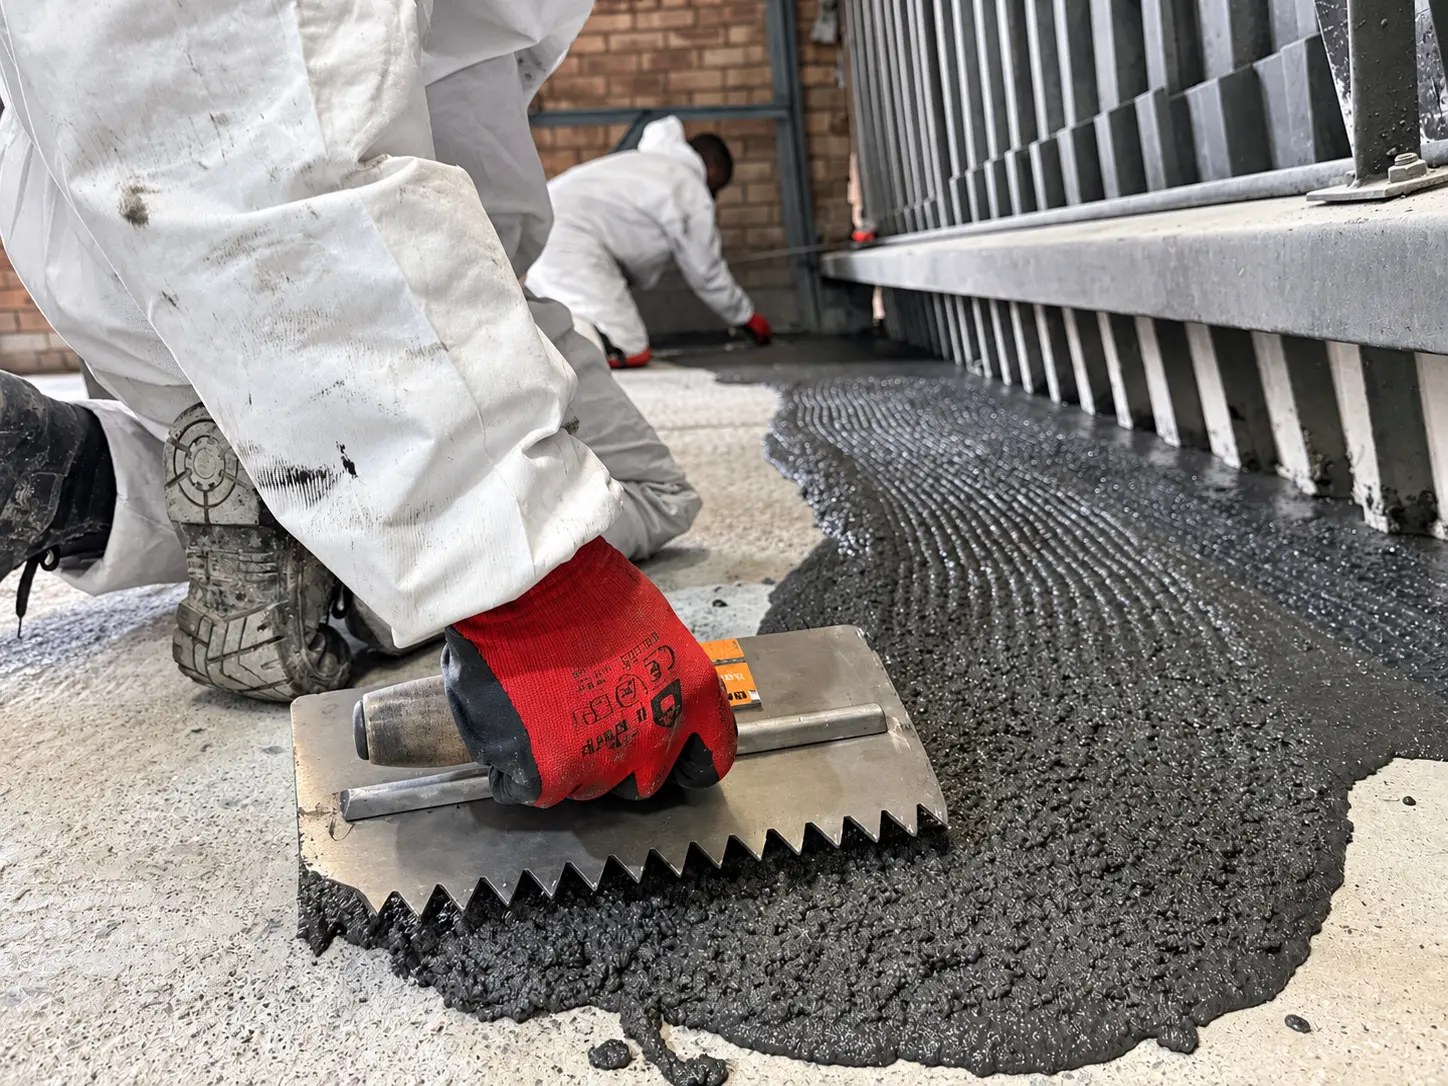
NUVO PROGROUT SL - NATURAL
6-LAYER CONSTRUCTION
Read More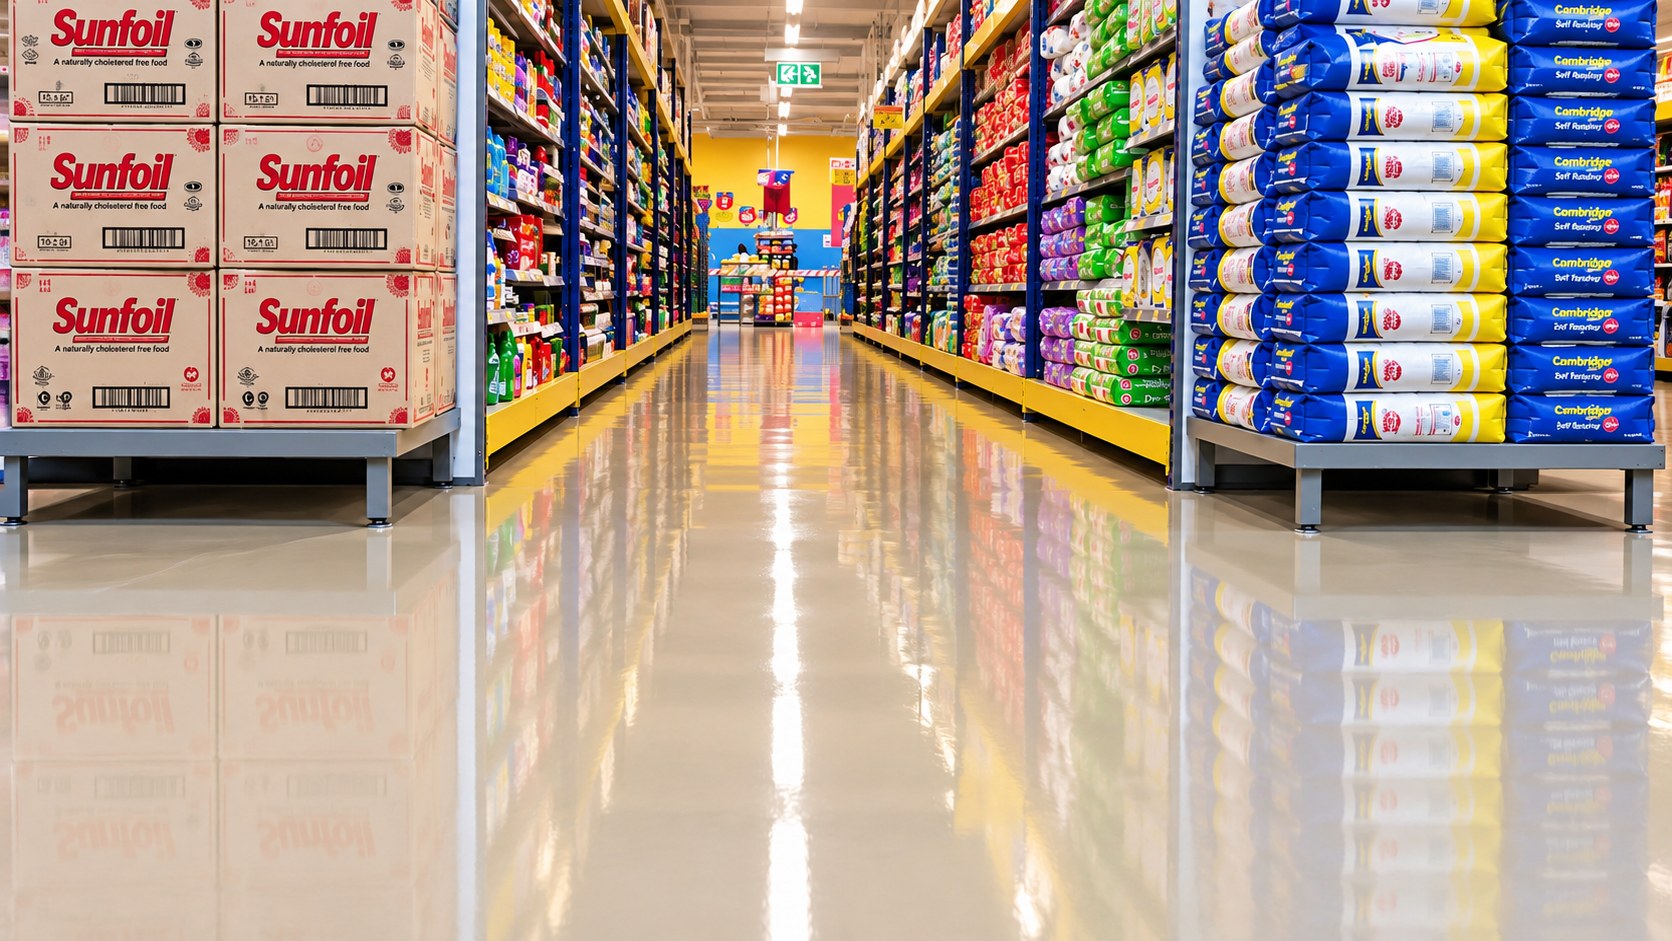
NUVO PROSEAL
EPOXY COATING SYSTEM — HIGH PERFORMANCE, SOLVENT FREE, PROTECTIVE COATING
Read More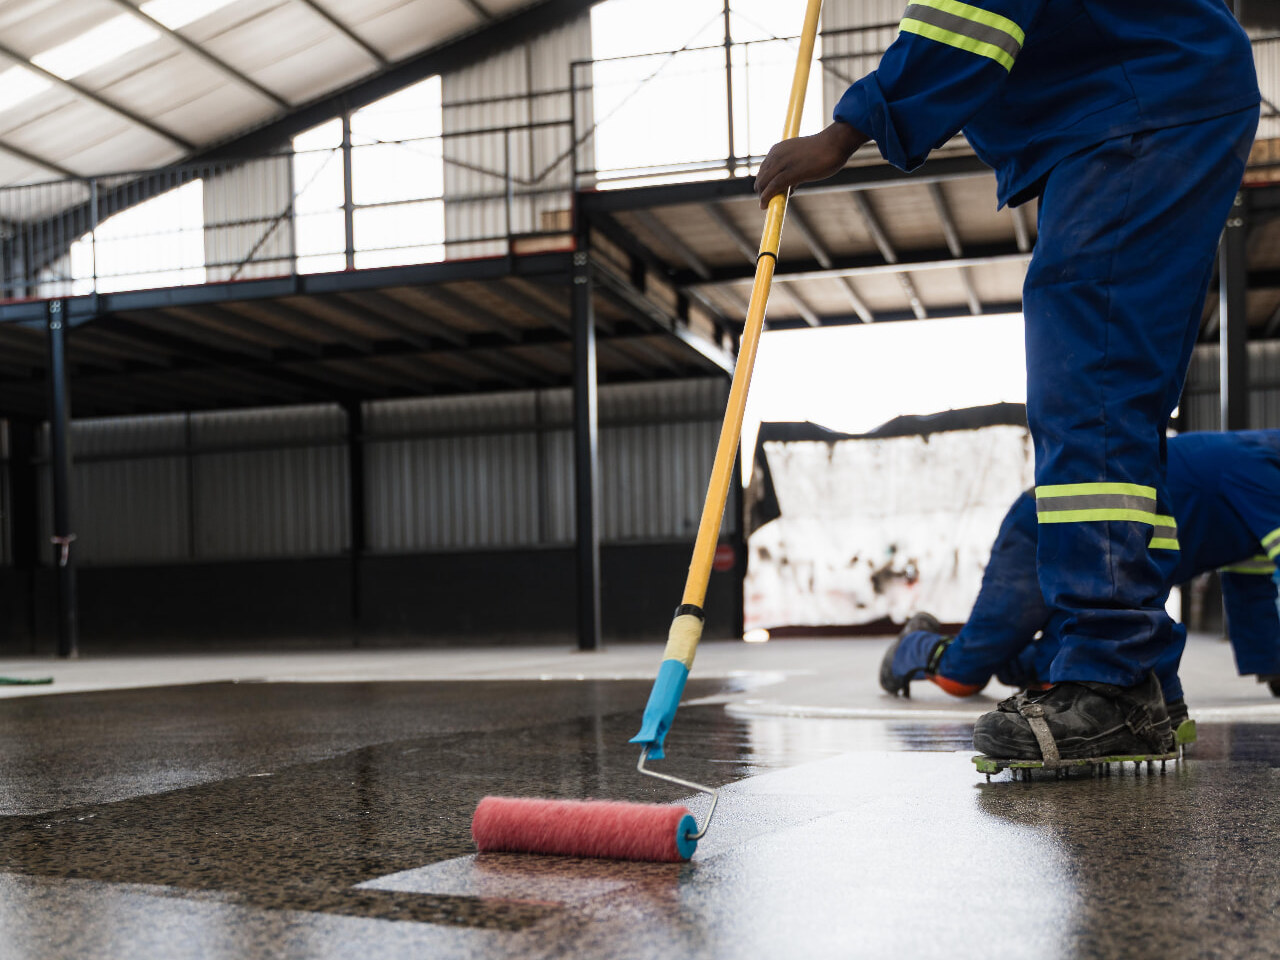
NUVO PROSEAL CLEAR
EPOXY COATING SYSTEM - CLEAR — HIGH PERFORMANCE, SOLVENT FREE, PROTECTIVE COATING
Read More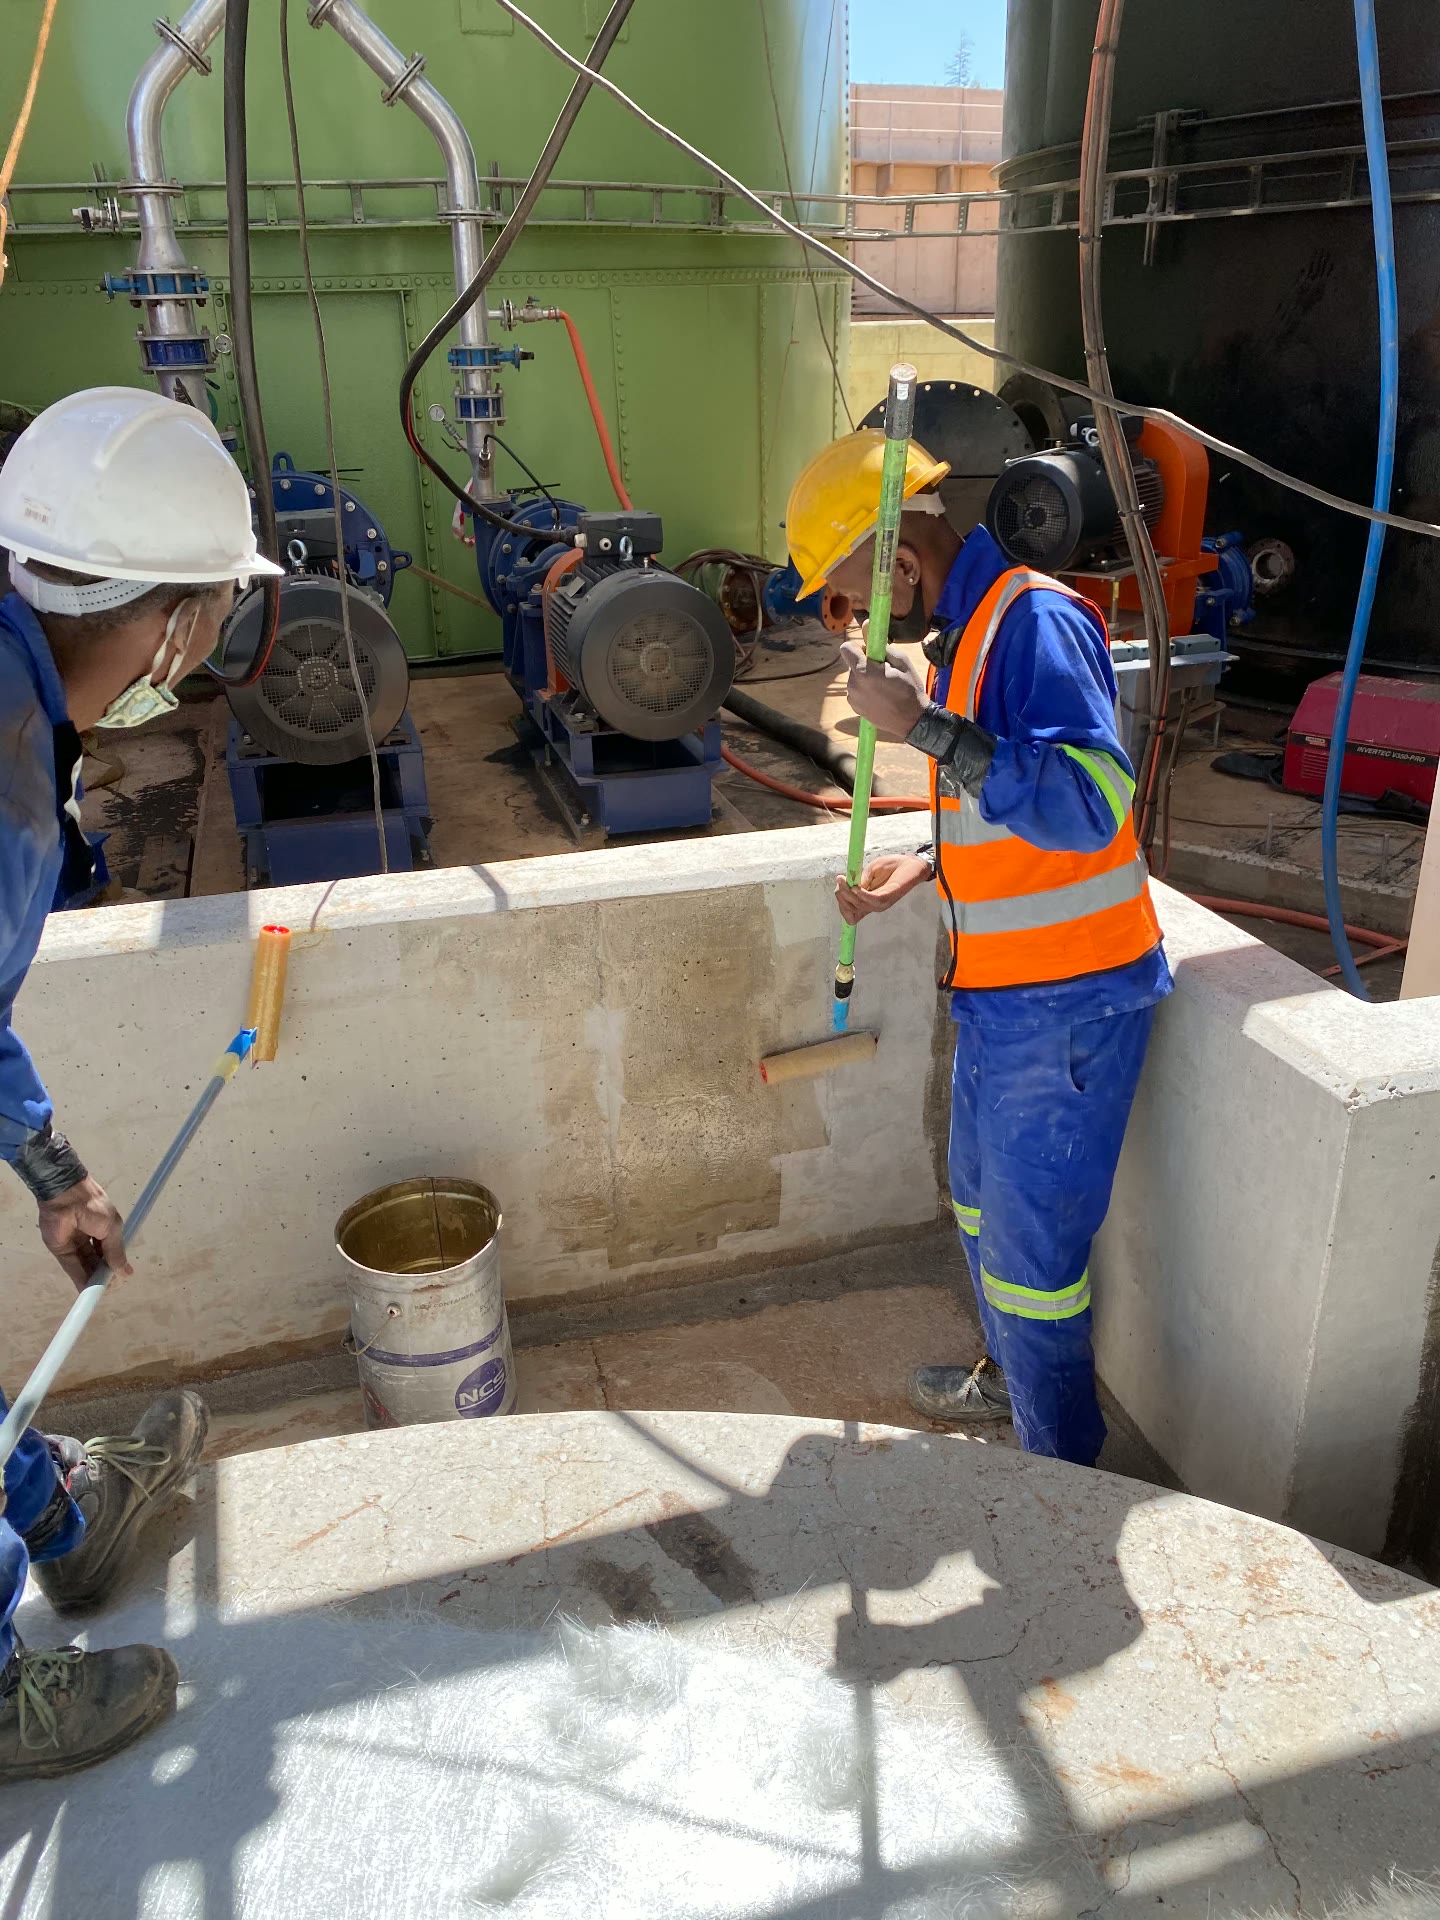
Industrial Acid-Proofing & Corrosion Protection
Concrete Bund Rehabilitation & Acid-Resistant Lining
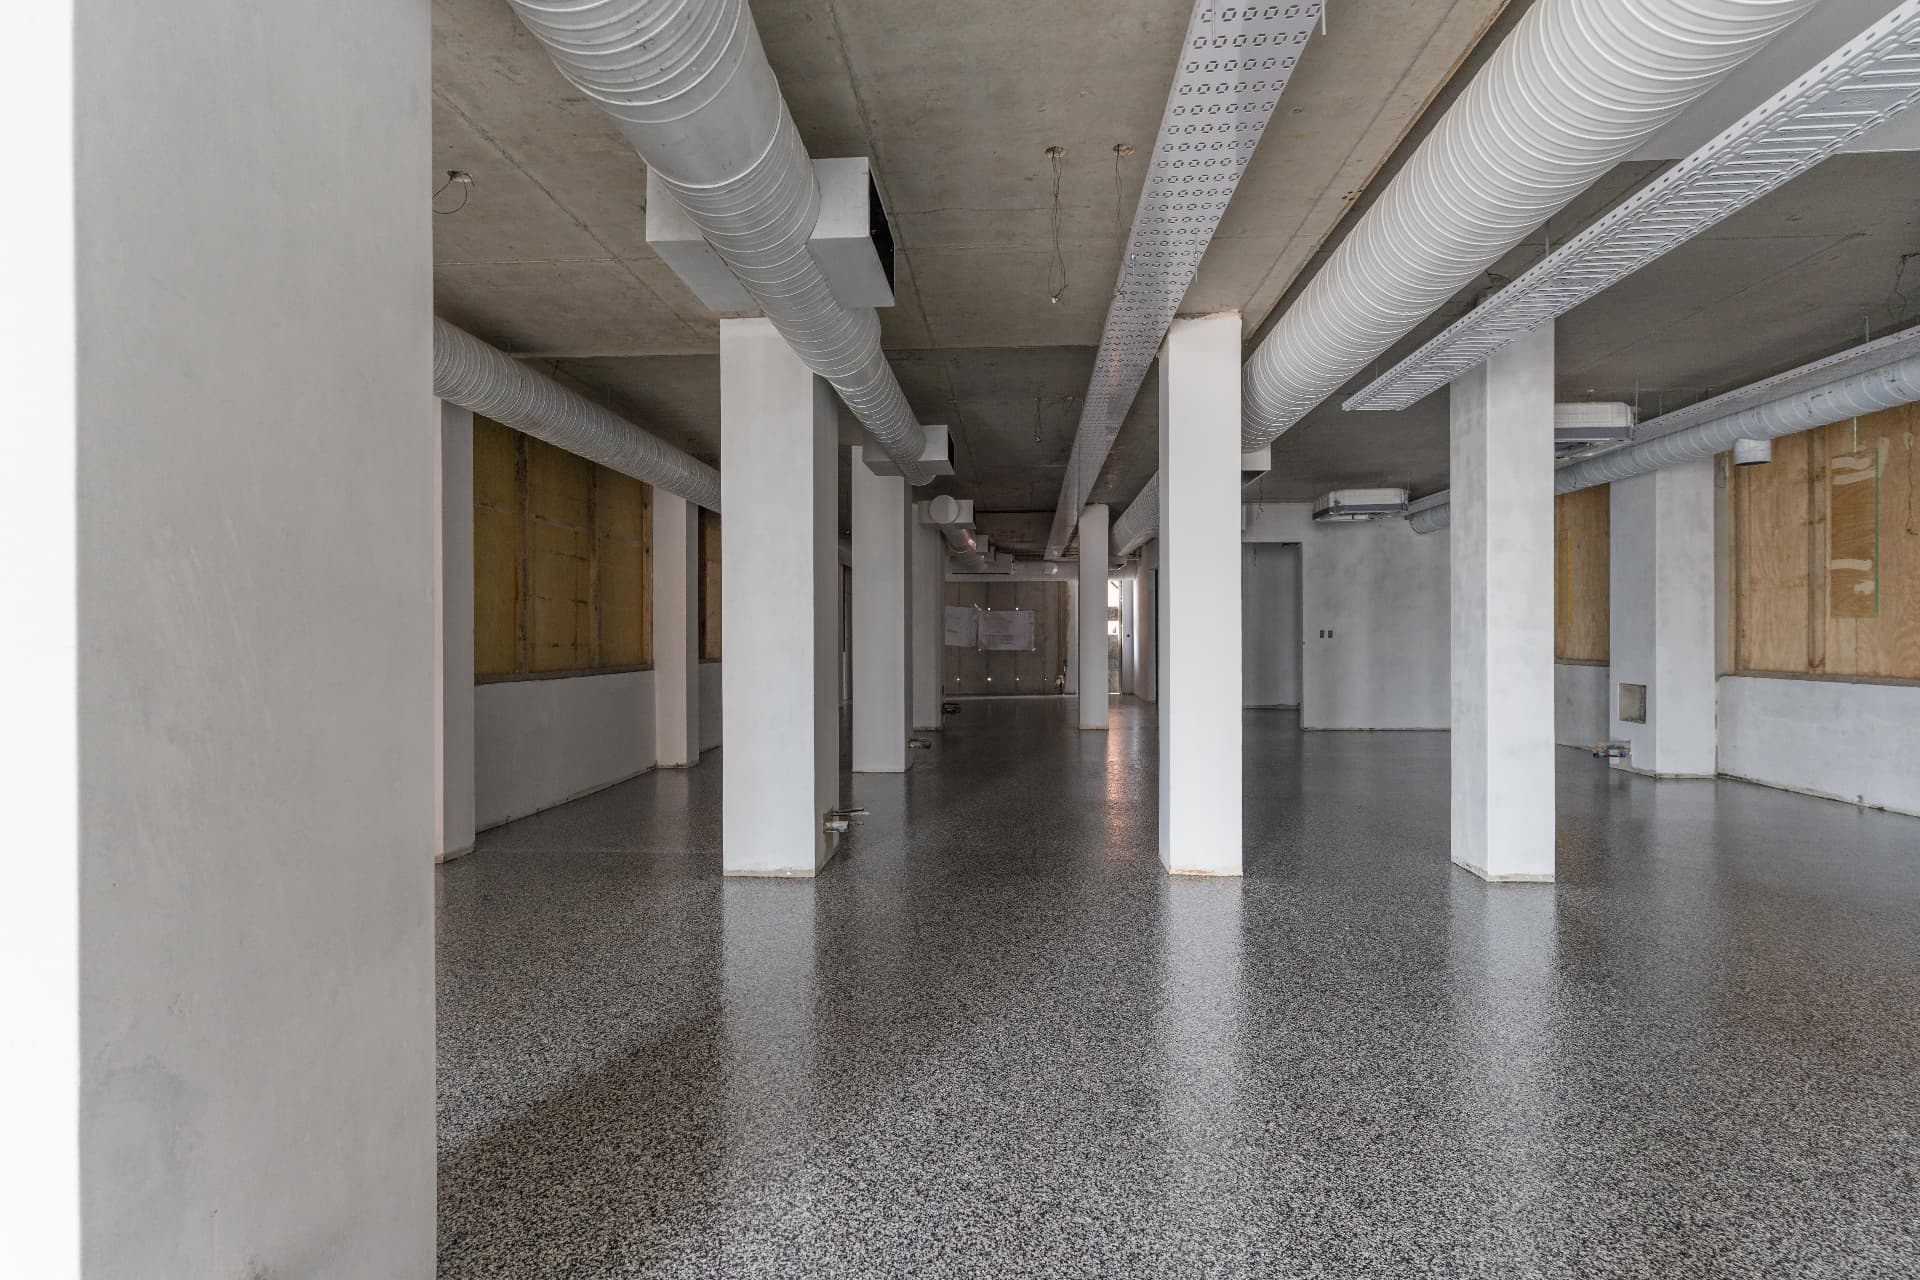
Food & Beverage Processing Facility
Industrial Flooring & Manhole Rehabilitation
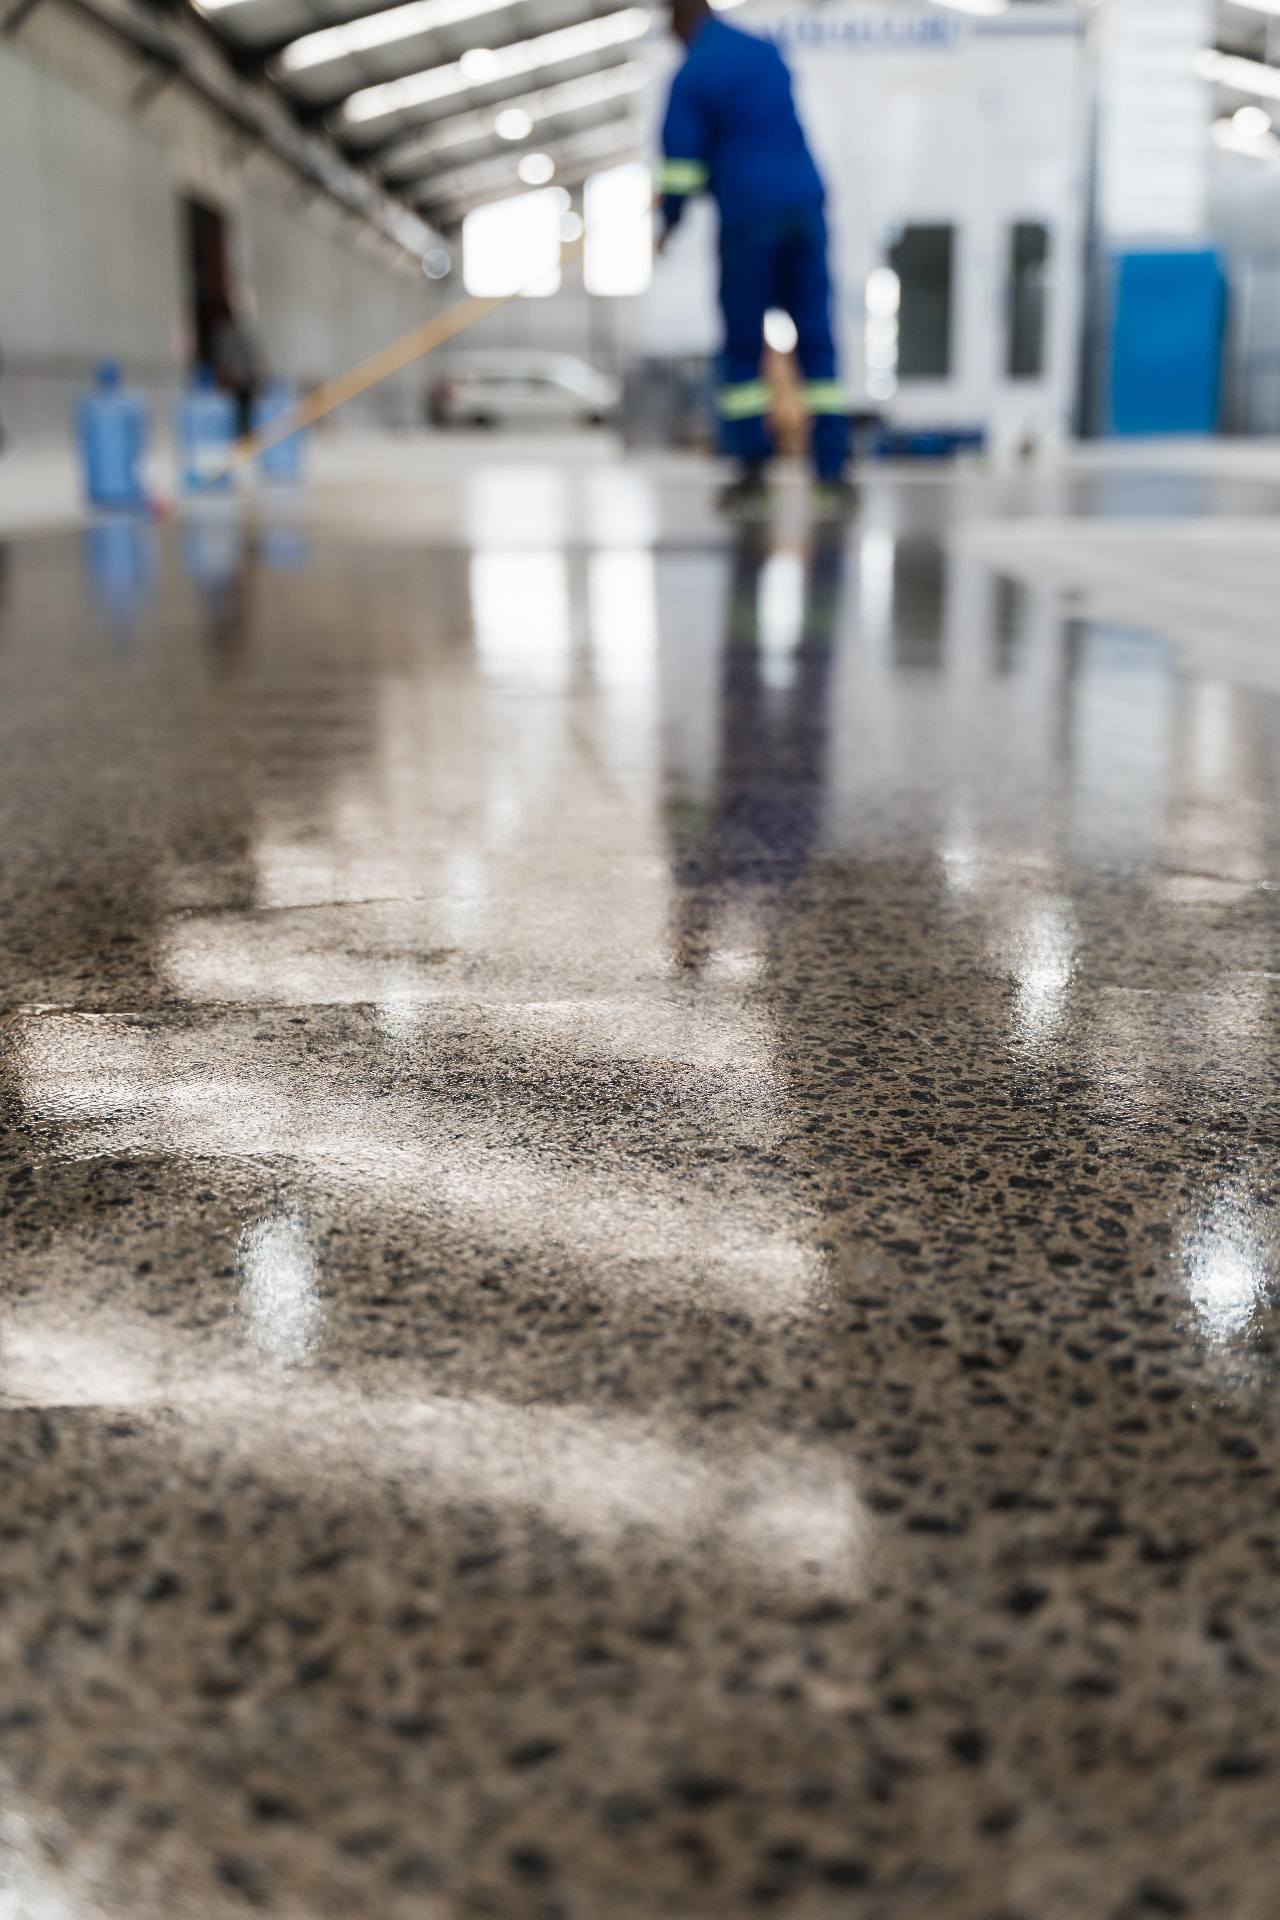
Industrial Concrete Grind & Seal
Concrete Surface Refinement & Protective Sealing